www.industryemea.com
14
'26
Written on Modified on
Ethernet-APL Deployment in Industrial Zinc Processing
ABB and Boliden integrate Ethernet-APL field instrumentation with System 800xA at Kokkola to enhance diagnostics and preserve installed automation infrastructure.
global.abb
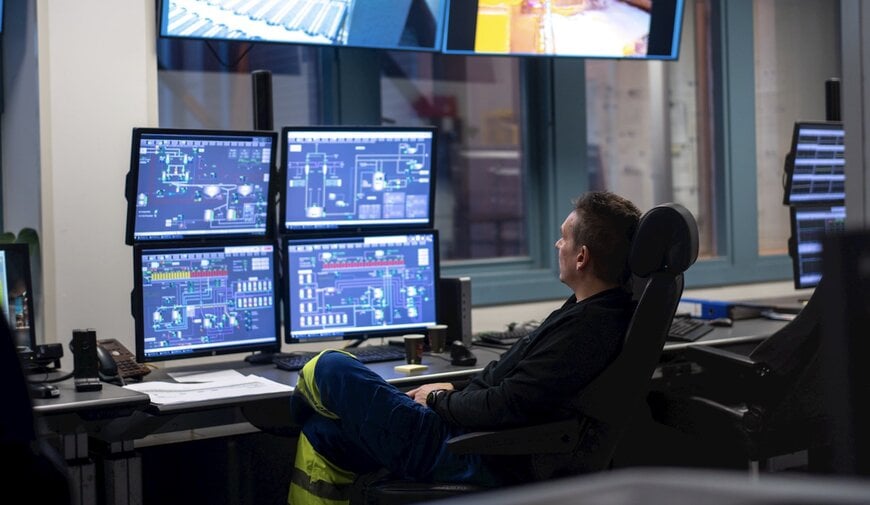
Process metallurgy and heavy industrial refining facilities require real-time visibility into process parameters and field instrument health to reduce unplanned downtime and optimize throughput. For decades, processing sites have relied on analog 4-20 mA with HART or legacy fieldbus networks. While dependable, these technologies impose bandwidth limits that constrain deep digital diagnostics and necessitate costly manual interventions in hostile plant areas. Completely replacing operational field wiring and control networks, however, introduces unacceptable downtime and high capital expenses. Modernizing process instrumentation demands a migration path that brings high-speed digital connectivity to field devices without requiring a rip-and-replace overhaul of plant automation.
Architecture and Physical-Layer Modernization
Boliden Kokkola, operator of a major zinc processing facility in Finland, addressed these constraints by deploying Ethernet Advanced Physical Layer (Ethernet-APL) field devices connected to its existing ABB Ability System 800xA distributed control system. Implemented in partnership with Pepperl+Fuchs, the installation represents one of the earliest industrial-scale deployments of the technology in Finland.
The deployment integrates Ethernet-APL hardware alongside existing Profibus PA field instruments on the same automation platform. By eliminating the need for a total infrastructure overhaul, the network design allows the operator to phase in high-bandwidth field devices at an operational pace that aligns with standard maintenance windows.
Centralized Field Management and Device Telemetry
To supervise both legacy and high-speed field devices, the Kokkola installation incorporates a pilot run of the ABB Ability Field Information Manager. Integrated directly into the System 800xA architecture and the Ethernet-APL network, the manager unifies configuration, monitoring, and parameterization workflows across mixed communication protocols.
This unified view extracts real-time process data and granular diagnostics directly from field devices into the main control room. Maintenance crews can detect early signs of instrument degradation, sensor drift, and valve wear remotely. By diagnosing issues from the control environment, the facility reduces manual technician sweeps in harsh production environments and lays the groundwork for centralized remote operations.
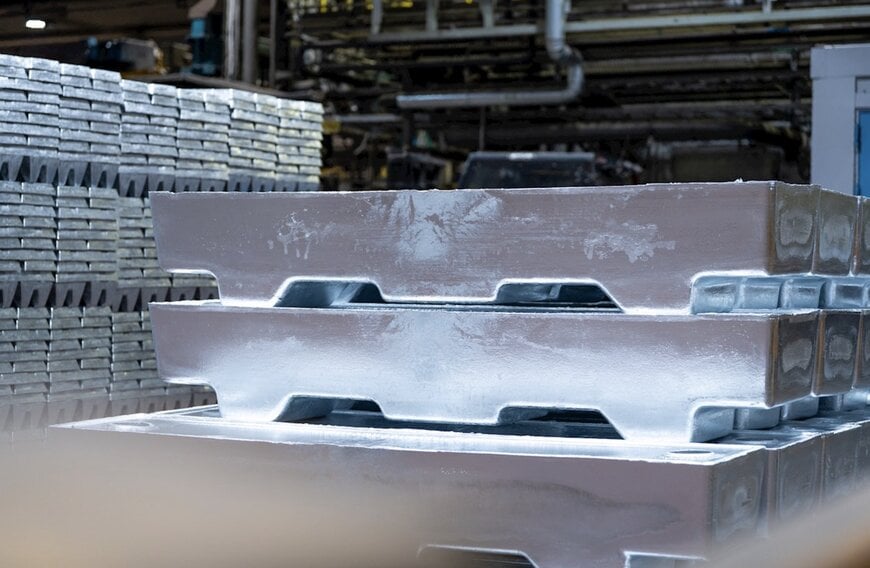
The automation partnership with ABB supports the production of zinc slabs at Boliden's Kokkola plant. Image Boliden
Long-Term Infrastructure Scalability
The Kokkola deployment extends an automation partnership between ABB and Boliden that started in 2014 during the construction of a silver recovery facility. Over the intervening years, the System 800xA control backbone has expanded across the broader zinc refinery. Because the system provides native protocol support for Profibus, Profinet, Ethernet-APL, and third-party systems, it allows next-generation digital standards to operate concurrently with installed field equipment throughout multi-decade asset lifecycles.
Additional Context
This section details technical specifications and competitive benchmarking not included in the original product announcement.
Ethernet-APL defines an enhanced physical layer based on the IEEE 802.3cg (10BASE-T1L) single-pair Ethernet specification, delivering 10 Mbps full-duplex communication alongside power delivery over a single twisted-pair cable. In contrast to legacy Profibus PA or Foundation Fieldbus H1 architectures—which operate at 31.25 kbps—Ethernet-APL increases transmission bandwidth by over 300 times. This speed jump enables continuous transmission of high-density diagnostics, device configuration parameters, and multi-variable sensor arrays without degrading real-time control loops.
The physical specification incorporates intrinsic safety via the 2-Wire Intrinsically Safe Ethernet (2-WISE) standard defined in IEC TS 60079-47, permitting deployment in Zone 0, Zone 1, and Division 1 explosive atmospheres. Ethernet-APL supports trunk topologies up to 1,000 meters in Zone 1 / Division 2 and spur segments up to 200 meters into Zone 0 / Division 1. Furthermore, because the physical layer complies with standard IEEE 802.3 Ethernet, it carries native industrial Ethernet application protocols—such as PROFINET, EtherNet/IP, and OPC UA—directly to the field instrument, flattening the classical automation pyramid and eliminating intermediate protocol converter gateways.
Edited by Romila DSilva, Induportals Editor, with AI assistance.
www.abb.com